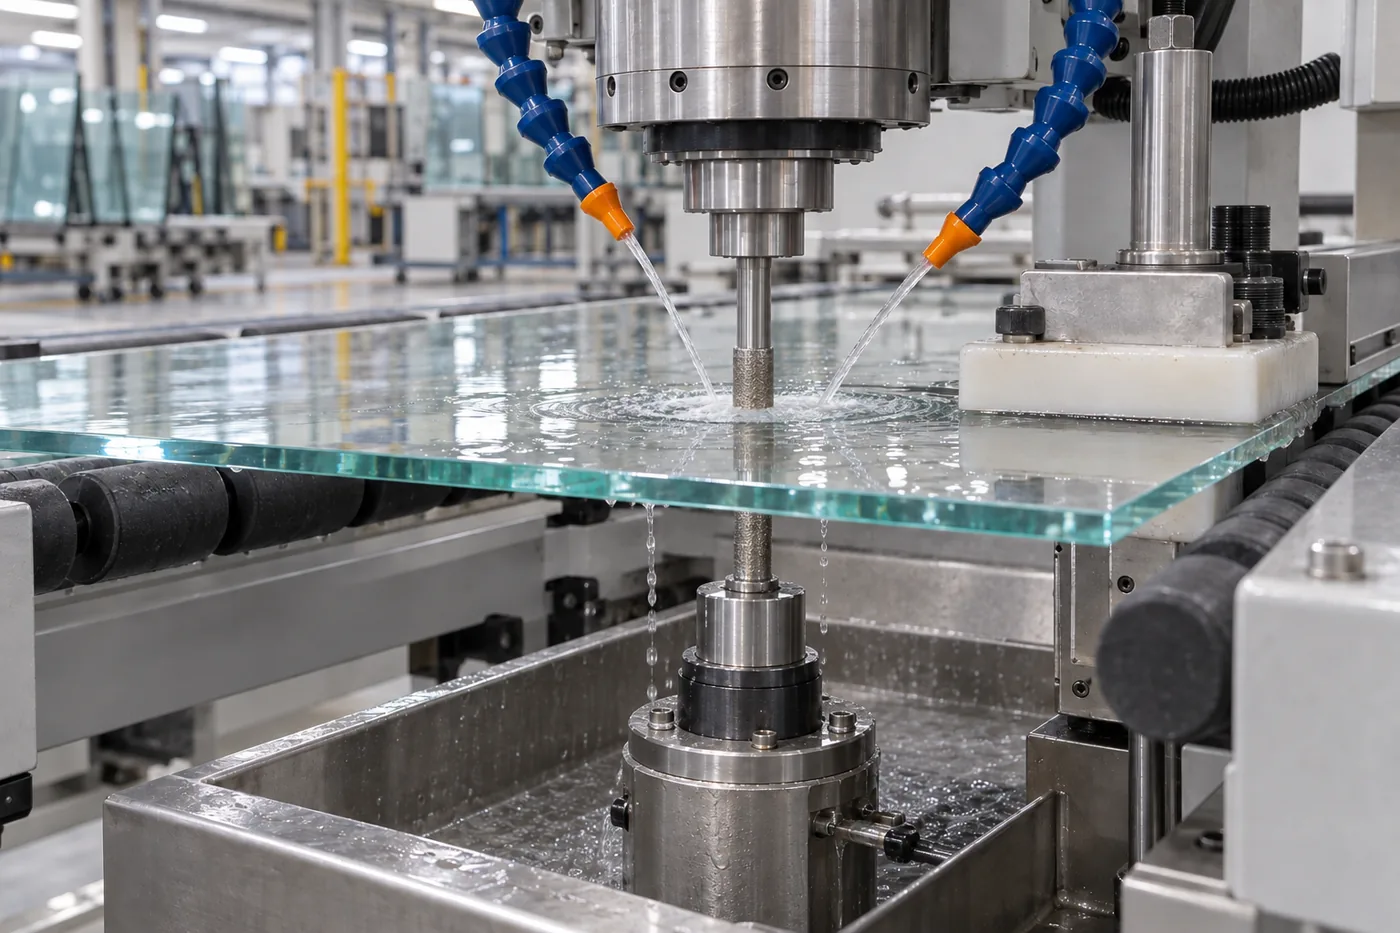
A shower enclosure is only as safe as its weakest cut edge. This guide looks at the glass itself — specifically why holes, slots, and notches are where tempered shower glass fails first, and what the Chinese national standard actually requires.
Why holes matter on tempered glass
Tempered glass gains its strength from a balanced stress field: the surface is held in compression while the core is in tension. Drill a hole or cut a notch into that field, and you create a stress concentration point. If the geometry is wrong, the glass may shatter inside the tempering furnace; if it passes the furnace, it may still self-destruct months later under thermal cycling or a light bump.
This is not a quality-control issue you can fix after tempering. All holes, slots, and notches must be cut and edged before tempering — never drill or cut tempered glass after it leaves the furnace.
The governing standards
- GB/T 15763.2-2025 Safety glass for building — Part 2: Tempered glass (replaces the 2005 version)
- GB/T 36266-2018 Tempered glass for shower enclosures
- Industry tempering-furnace practice sets tighter internal limits than the national standard.
Hole position — the numbers that matter
These are Chinese standards. US safety-glazing standards (ANSI Z97.1, CPSC 16 CFR 1201) test impact performance and do not specify hole geometry; the hole rules below are standard fabrication practice worldwide. Per GB/T 15763.2-2025, for glass thickness t:
| Dimension | Requirement | 8 mm (≈ 5/16 in) glass example |
|---|---|---|
| Hole edge to straight glass edge (a) | ≥ 2 t | ≥ 16 mm (≈ 5/8 in) |
| Clear distance between two hole edges (b) | ≥ 2 t | ≥ 16 mm |
| Hole edge to glass corner (c) | ≥ 6 t | ≥ 48 mm (≈ 1-7/8 in) |
| Hole diameter (D) | ≥ t | ≥ 8 mm |
| Hole edge chamfer | ≥ 1 mm (≈ 0.04 in) | ≥ 1 mm |
There is one special clause buyers often miss: if c (hole-to-corner distance) is less than 35 mm (≈ 1-3/8 in), the hole center must NOT lie on the corner bisector — it has to be offset. Placing a hole symmetrically in a corner is a classic self-break recipe.
Notches and cut-outs — no sharp corners allowed
The national standard does not give a numeric fillet radius for notches, but every tempering furnace manufacturer rejects parts with sharp internal corners. The industry rule is:
| Feature | Requirement | 8 mm glass example |
|---|---|---|
| Internal notch corner (concave) | Fillet radius R ≥ t | R ≥ 8 mm |
| Irregular hole corner | Fillet radius R1 ≥ t | R1 ≥ 8 mm |
| Outer glass corners | No sharp edges, chips, or cracks | Chamfer or round |
| Hole edge | Must be chamfered ≥ 1 mm | Mandatory |
A 90° internal notch angle is the single most dangerous feature on a shower door. Furnace operators will either refuse to temper it or charge a high rejection rate. Design it with a proper radius.
Zenova internal specification
The GB minimums are legal floors. For our own 8 mm shower glass, Zenova designs to:
| Feature | GB minimum | Zenova internal (8 mm glass) |
|---|---|---|
| Hole to straight edge (a) | 2 t | ≥ 2 t (16 mm) |
| Clear distance between holes (b) | 2 t | ≥ 2 t (16 mm) |
| Hole to corner (c) | 6 t | ≥ 6.5 t (~52 mm ≈ 2-1/16 in) |
| Hole diameter (D) | ≥ t | ≥ 1.25 t (10 mm ≈ 3/8 in) |
| Notch internal radius (R) | R ≥ t | R ≥ t (8 mm) |
| Hole edge chamfer | ≥ 1 mm | ≥ 1 mm (mandatory) |

Surface stress caveat
For unperforated flat tempered glass, China's GB/T 15763.2-2025 requires surface stress ≥ 90 MPa; the US standard ASTM C1048 requires ≥ 69 MPa (10,000 psi) for fully tempered glass. Zenova tempers to the 90 MPa requirement. Our tempered glass is produced by safety-glazing manufacturers certified to ANSI Z97.1-2015 and CPSC 16 CFR 1201 — see our Certifications page for the certificate holders and numbers. For glass with holes, slots, or notches, the standard does not set a single number — the stress field is no longer uniform, and the value must be agreed between buyer and tempering supplier. Do not accept a generic "≥ 90 MPa" certificate on perforated glass; ask for a batch-specific report.
Bottom line for your next PO
- All holes, slots, and notches before tempering — never drill or cut tempered glass post-furnace.
- Specify hole-to-edge ≥ 2t, hole-to-corner ≥ 6t, and hole diameter ≥ 1.25t in writing.
- No sharp internal corners on notches; fillet radius R ≥ t on all concave cut-outs.
- Hole edges chamfered ≥ 1 mm on both sides.
- For perforated glass, agree the surface-stress value with your tempering supplier per batch — do not rely on the generic 90 MPa figure.
— The Zenova Engineering Team, Zhongshan, China